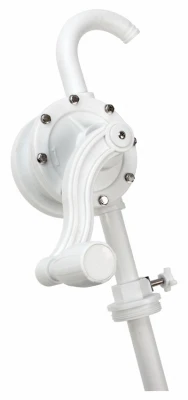
Introducing the Heavy‑Duty Rotary Barrel Transfer Pump, a rugged solution designed for swift and secure movement of Diesel Exhaust Fluid, gasoline, and a wide spectrum of industrial liquids. Its reinforced polypropylene body paired with PTFE‑coated vanes offers superior resistance to corrosive chemicals, while the compact hand‑lever mechanism snugly fits standard 5‑ to 55‑gallon containers. Each rotation delivers a steady flow, making fleet maintenance and equipment refueling faster and cleaner. Experience effortless fluid handling with a pump built for demanding environments.
Why Choose This Pump: Engineered for reliability, this rotary pump eliminates cross‑contamination with an integrated one‑way check valve, safeguarding product purity. The ergonomic lever action reduces fatigue, allowing operators to transfer up to seven gallons per hundred turns with consistent accuracy.
Key Features & Benefits:
- Robust Polypropylene Construction: Provides long‑lasting durability and chemical resistance for industrial fluid transfer.
- PTFE‑Lined Vanes: Enhances performance when handling acidic, alcoholic, or oil‑based liquids.
- Universal 5‑55 Gallon Compatibility: Fits standard pails and drums with a common bung fitting for versatile use.
- Hand‑Operated Rotary Lever: Delivers approximately 7 gallons per 100 revolutions, ensuring efficient, low‑effort operation.
- One‑Way Check Valve: Prevents backflow and protects against product contamination during transfers.
Final Thoughts: This heavy‑duty rotary barrel pump stands out as the go‑to tool for technicians, fleet managers, and workshop owners who demand speed, safety, and chemical resilience. Its thoughtful design merges durability with user‑friendly operation, delivering reliable performance across a broad range of fluids. Trust this pump to keep your operations flowing smoothly and your fluids pristine.
WARNING: Cancer and Reproductive Harm www.P65Warnings.ca.gov